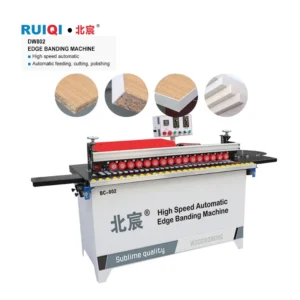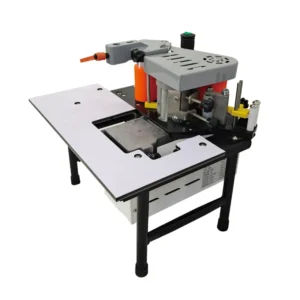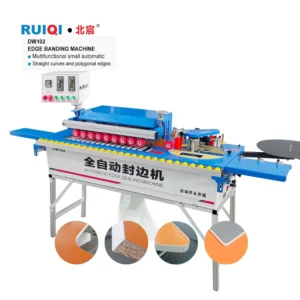

EDGE BANDING MACHINE


XZF450 Automatic Edge Banding Machine, 9.5KW, 0–12 m/min Feed, 0.3–3mm Edge Thickness — engineered as a line-integrated station with 7 functions including pre-milling, 30/45/60° edging, trimming, scraping and polishing. Feed speed and infeed height match upstream panel saws and downstream boring machines for balanced material flow across cabinet production lines.
Configured For Line Integration — feed speed, infeed height, and electrical specs matched to upstream and downstream stations before the edge banding machine production line ships.
| Parameter | Value |
|---|---|
| Model | XZF450 |
| Product Type | Automatic Edge Banding Machine |
| Total Installed Power | 9.5 kW |
| Pre-milling Motor | 4 kW |
| Trimming Motors | 2.2 kW × 2 |
| Polishing Motors | 0.4 kW × 2 |
| Vacuum Extraction | 550 W |
| Transmission Drive | 180 W |
| Edge Feed Motor | 0.16 kW |
| Feed Speed Range | 0–12 m/min |
| Operating Voltage | 380V / 415V |
| Compressed Air Requirement | 0.5–0.7 MPa |
| Glue Pot Capacity | 4000 ml |
| Edge Banding Height | 0–50 mm |
| Edge Banding Thickness | 0.3–3 mm |
| Minimum Panel Length | 300 mm |
| Minimum Panel Width | 150 mm |
| Machine Footprint | 3000 × 650 × 1350 mm |
| Net Weight | 430 kg |
| Application | Material or Output |
|---|---|
| Cabinet door and carcass edging | MDF, melamine-faced chipboard, plywood |
| Office furniture panel finishing | Particleboard, blockboard with PVC or veneer banding |
| Polymer door production | Polymer sheets, MDF substrates with 0.3–3 mm edge material |
| High-volume residential cabinet runs | Solid wood panels requiring 30°, 45°, or 60° angled edging |
| Panel furniture production line integration | Board stock sized above 300 × 150 mm minimum dimensions |
A 0–12 m/min variable feed range only matters if the upstream panel saw and downstream boring stations are configured to match — without that coordination, panels queue and shifts stall.
Buying a standalone edge banding machine without confirming how its feed speed aligns with the rest of the floor is one of the most common mistakes in furniture factory planning. We have seen cabinet manufacturers in Southeast Asia install automatic edgers that could not keep pace with their CNC saws, forcing panels to pile up on roller tables and creating a bottleneck that idled the downstream drilling operator for minutes every cycle [NEED_CITE: production line throughput synchronization practices]. The edge banding machine production line concept exists precisely to prevent that mismatch, ensuring each station passes work to the next without accumulation or starvation.
The XZF450 runs at a variable 0–12 m/min, which gives production planners the range needed to synchronize with typical panel sizing saws feeding cut boards at intervals. When we configure an edge banding machine production line, we calculate the panel flow rate from the saw based on average cut cycle times and board dimensions, then set the bander feed speed to absorb that flow with a small buffer. This prevents both starvation — where the bander runs empty waiting for the next panel — and accumulation, where boards stack against the infeed fence.
The 4000 ml glue pot capacity supports extended running between refills, which matters on longer production shifts where stopping to top up adhesive would disrupt the flow rhythm established with upstream equipment. A smaller pot would force more frequent pauses and shift the bottleneck upstream.
Panel transfer height between stations determines whether boards slide smoothly onto conveyor rollers or catch on a height mismatch that damages freshly cut edges. The XZF450 stands at a working height designed to align with standard roller conveyor systems used in cabinet and furniture manufacturing cells [NEED_CITE: industrial conveyor height standards for panel processing]. When we lay out a line, we specify the exact infeed and outfeed roller heights so that a panel exiting the panel saw transfers onto the bander without an operator lifting or guiding it manually.
This geometry check also extends to the outfeed side, where freshly banded panels must move to the boring station or stacking area without the fresh edge contacting a misaligned rail. Even a few millimeters of height difference can scrape the adhesive before it cures.
The 4 kW pre-milling motor provides enough torque to clean-shear the panel edge before glue application, which is critical when boards arrive from the saw with micro-chipping on melamine or veneer faces. Pre-milling removes this damage so the edge band sits flush, and the tolerance it achieves affects how accurately the panel fits into dowel or confirmat joints at the assembly stage downstream.
The trimming station uses two 2.2 kW motors running in sequence — one for the leading end, one for the trailing end — which gives clean perpendicular cuts on edge banding material up to 3 mm thick. This matters on a line because poorly trimmed ends create catch points that can jam the next panel behind it if the banding tail extends even slightly past the board edge.
The air source pressure range of 0.5–0.7 MPa must be matched to the factory’s central compressed air system. A shared compressor feeding multiple machines on the line can experience pressure drops when pneumatic cylinders on several stations actuate simultaneously, so we verify that the edge bander receives stable pressure within spec even at peak demand [NEED_CITE: pneumatic pressure stability requirements in multi-station woodworking lines].
Factories that buy edge banders, saws, and boring machines from separate suppliers without a unified layout often discover incompatibilities only after installation. Feed heights that differ by a centimeter force operators to manually lift panels between stations, which slows the cycle and risks edge damage. Voltage mismatches discovered at commissioning mean rewiring or transformer installation before the machine can run. And an edge bander speced for lower volumes than the saw output will produce becomes a permanent constraint on the entire shift [NEED_CITE: common machinery integration failures in panel furniture factories]. These are not problems a single machine can solve after the fact — they require line-level planning from the quotation stage.
Every XZF450 destined for a production line is assigned a position in the layout drawing before production begins, with infeed and outfeed coordinates locked to adjacent stations. Our engineers calculate throughput compatibility using the actual panel sizes and edge banding specifications the factory will run, not generic assumptions. Voltage and frequency are confirmed against the entire line’s electrical specification — not just the edge bander in isolation — so that one unified control cabinet can serve all stations.
The four-stage quality control process includes a pre-shipment line test where the bander runs in sequence with the other configured machines to verify signal handoffs and material flow timing. Patented cutting mechanisms in the trimming station hold tolerances that assembly jigs downstream depend on. And the configuration recommendation is backed by a formal quotation that itemizes every station, so the buyer sees exactly how throughput is balanced before committing.
To configure the XZF450 as part of an edge banding machine production line that actually balances, we need your upstream panel saw model and its output rate, your planned panel size range and edge banding material, and the downstream boring station cycle time. Include your local voltage and frequency, and the available floor space with ceiling height so we can route conveyors properly. If you are phasing this into an existing line rather than building new, share the current conveyor heights and control system brand so we can verify integration points before shipping.
Q: How is the feed speed of this edge bander matched to upstream panel saws and downstream boring machines on the line?
A: We calculate the panel flow rate from your saw based on its cut cycle time and the average board dimensions you will run, then set the XZF450 feed speed within its 0–12 m/min range to absorb that flow. Downstream, we verify that the boring station cycle time can accept panels at the bander’s output rate without queuing. This calculation is included in the formal quotation.
Q: Can this machine be phased into an existing line, or does it require a full turnkey configuration?
A: The XZF450 integrates into existing lines provided the infeed and outfeed conveyor heights align and the compressed air supply meets the 0.5–0.7 MPa requirement. We need your current conveyor specifications and the adjacent machine models to verify compatibility. If heights or control signals do not match, we specify transition modules as part of the configuration.
Q: What is the infeed and outfeed height, and how does it align with the rest of the production line equipment?
A: Working height is configured during line layout to match your existing or specified roller conveyors and adjacent stations. We lock this dimension in the layout drawing before manufacturing begins. A mismatched height forces manual panel lifting between stations, which slows throughput and risks damaging freshly banded edges during transfer.
Q: How is voltage and control integration handled when the edge bander is specified as part of a complete line?
A: Voltage is confirmed at 380V or 415V to match the entire line’s electrical specification before production starts. For lines with centralized control, we coordinate the PLC signal protocol so the bander responds to start and stop commands from the main panel. Electrical schematics for all stations are cross-referenced in the documentation package shipped with the line.
* Detailed technical specifications vary by model. Contact us for the full parameter sheet and customization options.
Heavy-duty wooden crate with moisture-proof lining and steel strapping. Seaworthy standard for safe ocean freight.
Standard models: 15-20 working days. Custom OEM orders: 25-35 working days from deposit confirmation.
FOB Qingdao / Tianjin. EXW, CIF available. T/T, L/C, Western Union accepted. Flexible payment terms for long-term partners.
We export to 100+ countries across Europe (Germany, Spain, Italy), Americas (USA, Mexico, Brazil, Argentina), Southeast Asia (Vietnam, Indonesia, Thailand), Africa (Nigeria, Egypt, South Africa), and the Middle East. Full customs documentation and export compliance support included.
Your logo on machine body, control panel and packaging. Full white-label production available.
Support 110V/60Hz, 220V/50Hz, 380V/50Hz, 440V/60Hz and other local electrical standards.
Modify table size, motor power, cutting capacity and other parameters per your production requirements.
Control panel available in English, Spanish, French, Arabic, Russian and other languages on request.
Custom paint color, machine casing design and aesthetic modifications to match your brand identity.
Bundled tooling sets, spare parts kits, installation tools and custom accessories for your market needs.
Fill in your requirements and our sales team will respond within 24 hours with a formal quotation and full technical specifications.